



MOBILE RACK
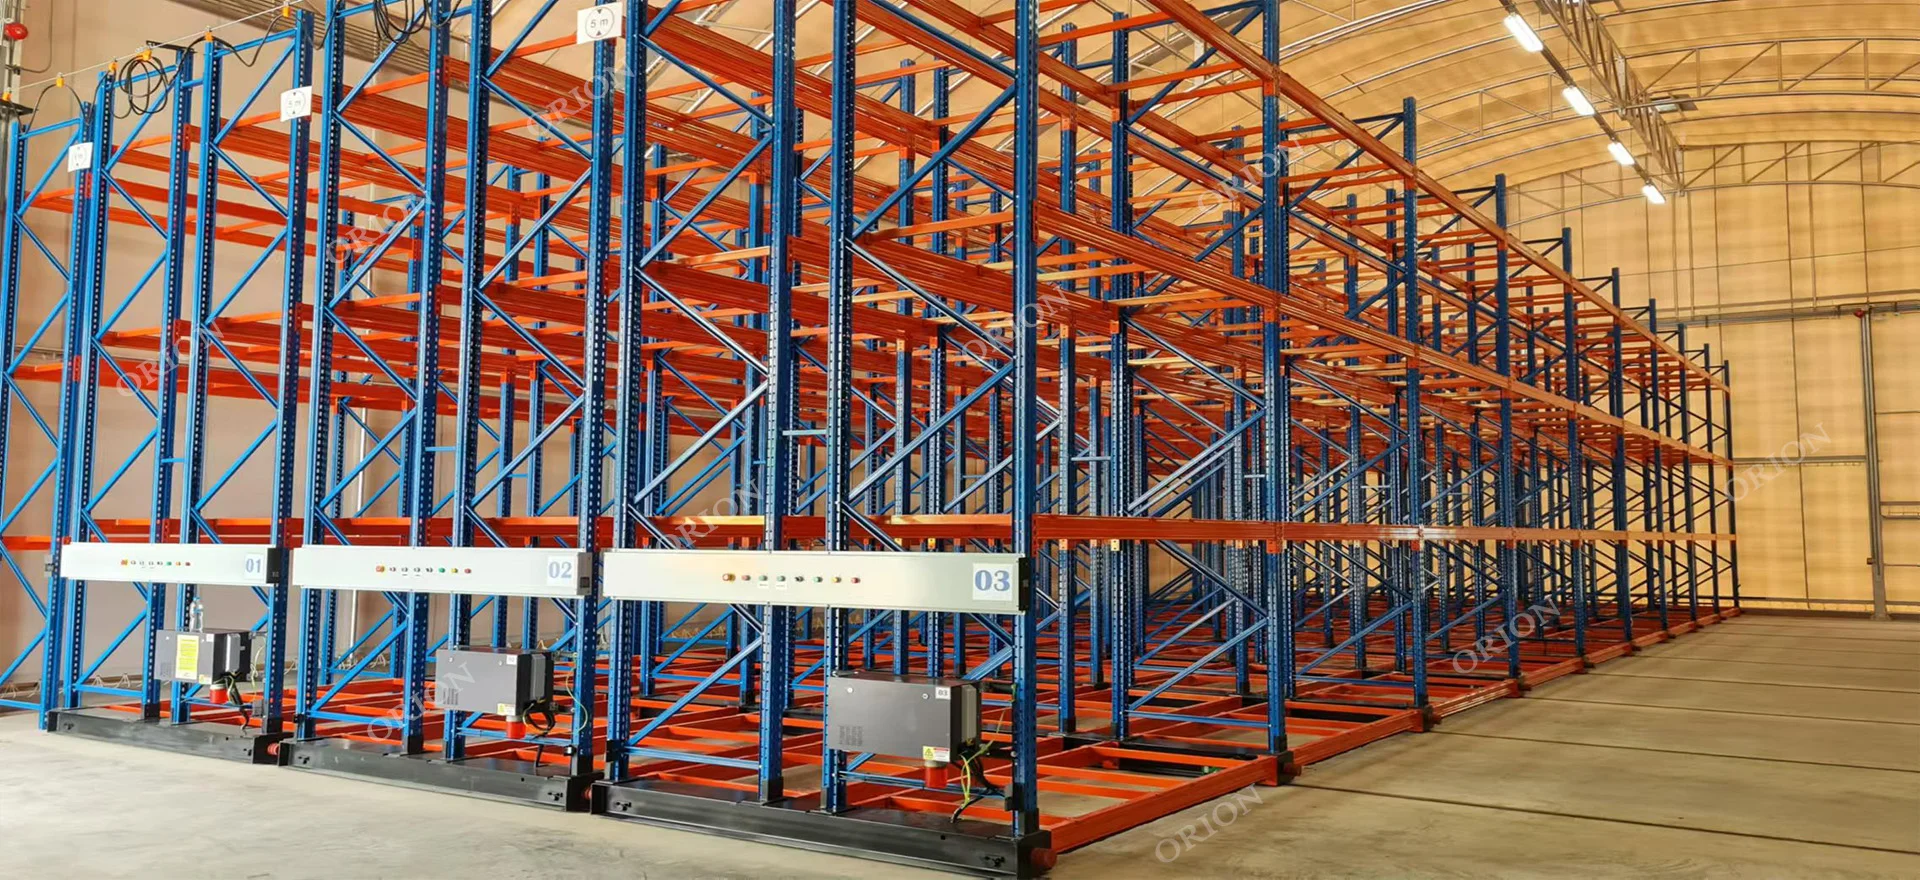
Mobile racking system maximizes warehouse storage capacity by eliminating fixed aisles. Ideal for cold storage, food & beverage and bulk inventory storage.
PRODUCT INTRODUCTION
Mobile Rack:
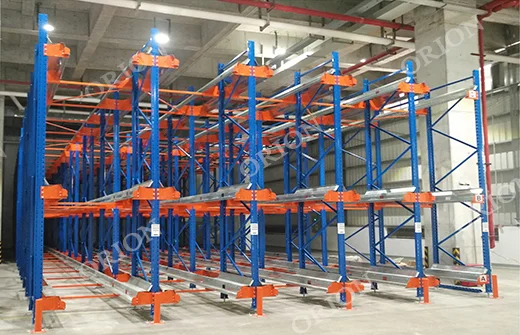
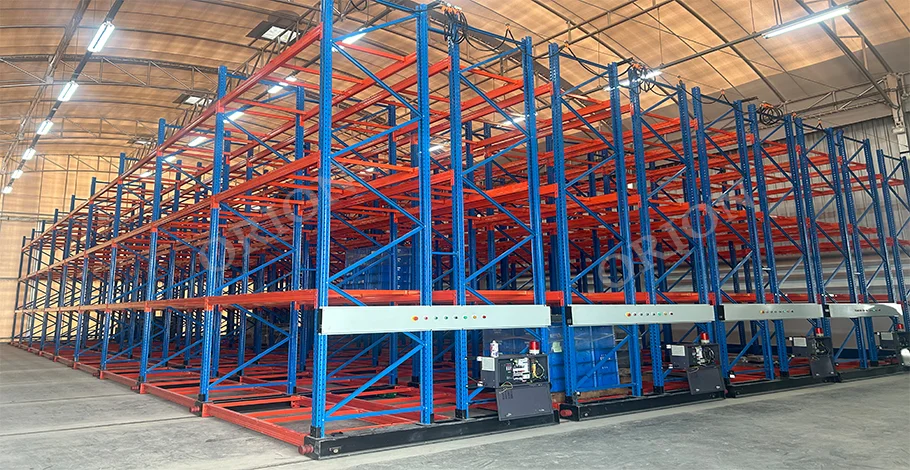
Mobile racking is developed based on conventional pallet racking. Two rows of racks are installed back-to-back on motorized mobile bases and arranged in groups. Controlled by buttons, racks slide along floor tracks to open a single access aisle for forklift pallet handling.
The mobile rack system comes with infrared safety sensors. It automatically stops movement if people or forklifts enter the aisle during operation.
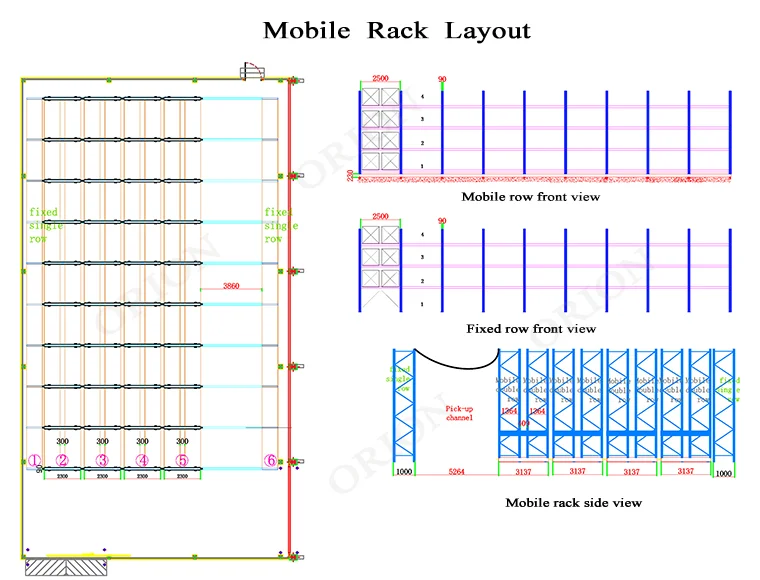
Only one working aisle required. It greatly boosts warehouse space utilization, with stable performance and simple operation. Ideal for multi-SKU warehouses with low to medium access frequency.
DESIGN FACTOR
| Space layout | According to the warehouse area to determine the layout and number of mobile shelves, make full use of space. |
| Load capacity | According to the weight of the goods to design the shelf’s load-capacity, including the load of each layer and the total load of the entire shelf. |
| Channel width | The channel width should meet the traffic requirements of handling equipment and goods size, but also make full use of warehouse space. |
| Length design | With the increase of shelf length, its stability will be affected to a certain extent. It is necessary to consider the warehouse space and also the stability of the shelves. |
| Mobility | Select the right mode of movement and drive. The common moving methods are manual, electric and so on. |
| Stability | In order to prevent the shelf from tilting during movement, stability measures need to be taken. |
| Safety | Not only to consider the safety of the shelf structure, but also to consider the personnel and goods. Set infrared sensor, set emergency stop button, etc. |
ADVANTAGES OF MOBILE RACKING
- Direct access: Each pallet can be accessed by moving shelves;
- High space utilization: There is only one channel, and other Spaces can be placed shelves to improve storage;
- Good safety: Multiple infrared sensors and Emergency stop are installed to ensure the safety of personnel in the operation of the shelf.
- Environmental protection and energy saving: Due to the reduction in the number of channels, the coverage area of facilities such as warehouse lighting and air conditioning is reduced, thus reducing energy consumption.
MOBILE PALLET RACKING APPLICATIONS
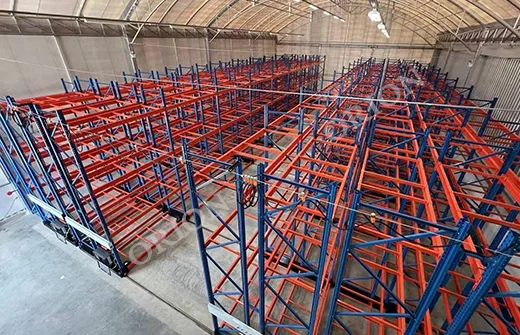
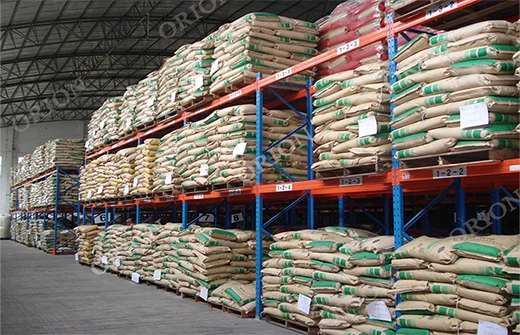
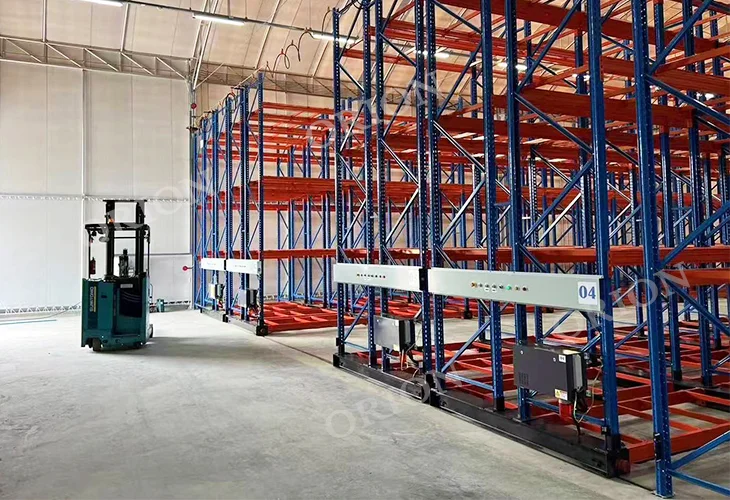
Variety of low turnover warehouse
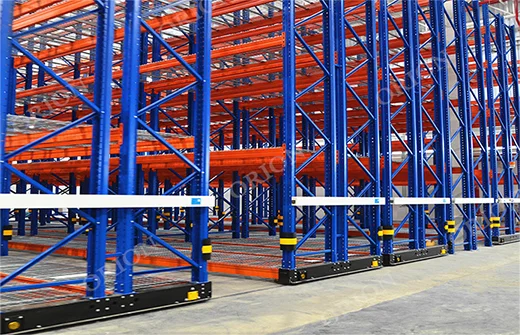
Warehouse with limited space
Mobile shelves can increase storage capacity.
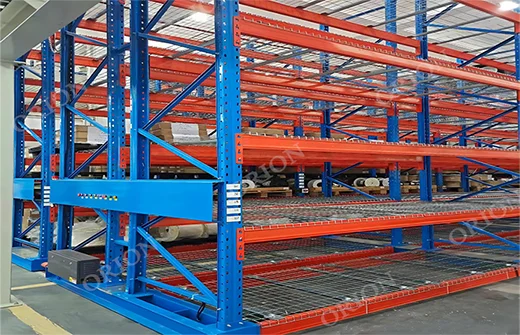
Cold Storage
Reduce cold storage space waste, reduce energy consumption.
MOBILE PALLET RACKING ACCESSORIES
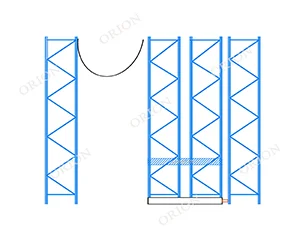
Rack
Similar to pallet rack, it usually contains moving columns and fixed columns.
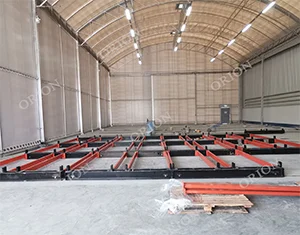
Base
Bearing shelf, include rolling wheel.
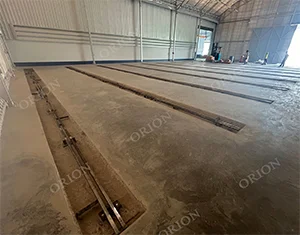
Track
The shelves move along the track.
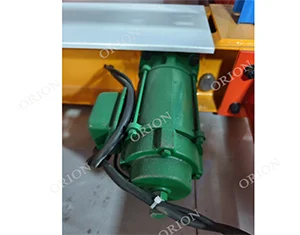
Motors
Provide power, motor power depends on the number of shelves and load bearing.
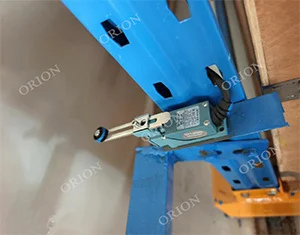
Position limit switch
Control the distance between shelves at the end of the run.
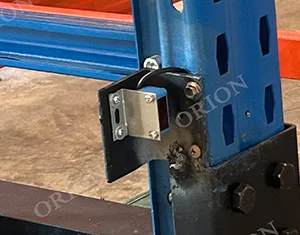
Infrared sensor
When the shelf is running, people or forklifts enter the channel, the shelf will automatically stop.
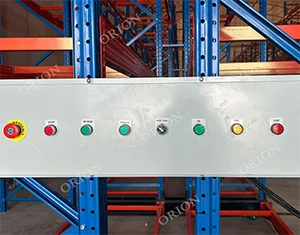
Control button/emergency stop button
Control the direction of shelf movement.
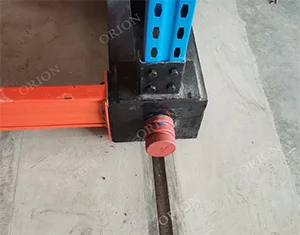
Anti-collision rubber
Prevent shelves from bumping into each other.
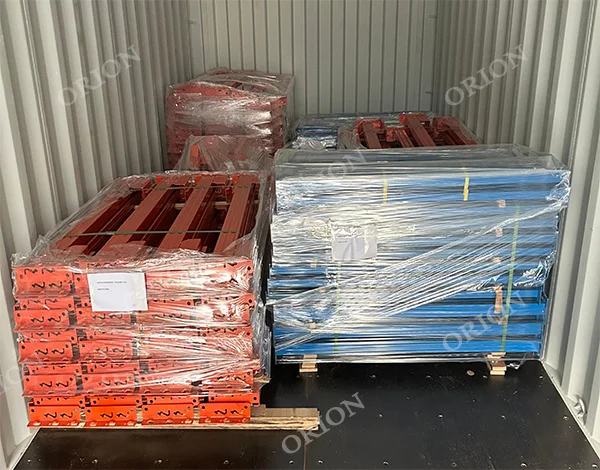
PACKAGING AND TRANSPORTATION
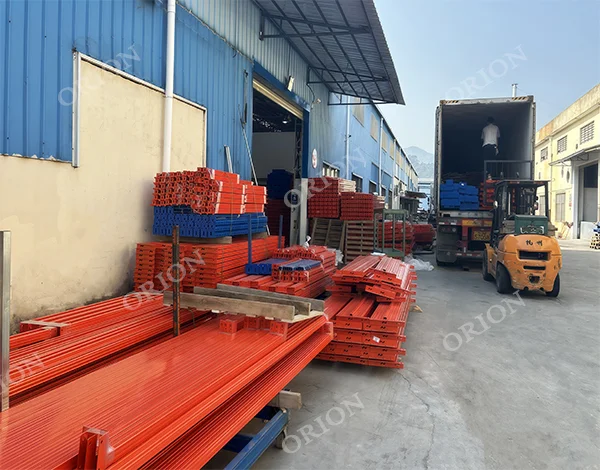
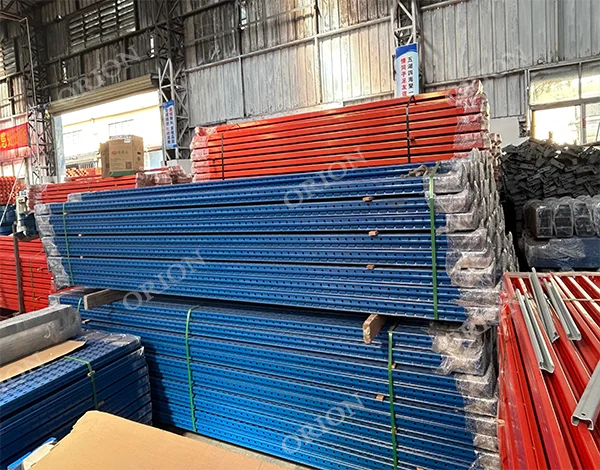
In order to ensure product quality and safety, different products have different packaging methods, commonly used wrapping film, bubble bag, carton, wood frame.

FAQS
Mobile shelf is a storage device that can be moved on a track. It consists of shelf, track and drive system.
There are two main types: manual and electric. Manual operation is suitable for light cargo. Electric drive with motor and control system, suitable for large warehouses, high frequency of use scenarios.
Mobile shelves through manual or electric drive, slide on the track, so that the multiple channels between the original multiple rows of shelves, into only one channel can access all the goods, greatly improving the space utilization rate.
Check the flatness of the warehouse ground to ensure that it meets the installation conditions; Install the track, accurately calibrate the levelness; Main shelf installation; Install and debug the drive system; Final overall inspection.
High space utilization, flexibility, storage security.
The initial investment cost is high; the ground requirements are high,;the maintenance requirements are many;and the spatial layout flexibility is limited.
Warehousing and logistics industry, manufacturing industry, electronic and electrical industry, etc.